

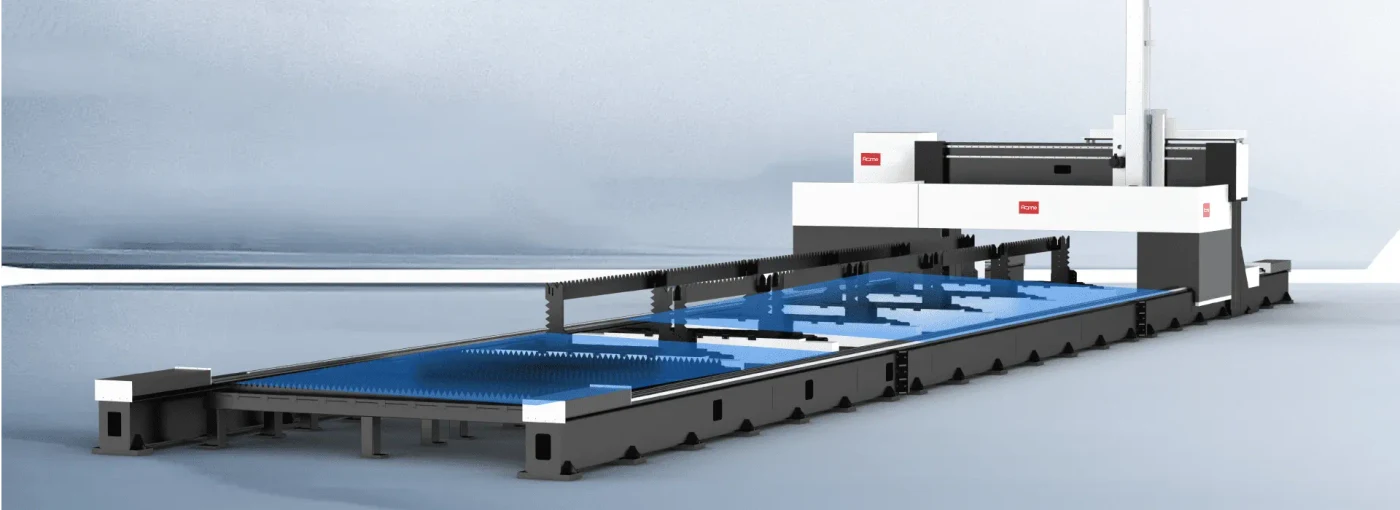
LHM Series — Gantry laser machine for heavy profiles and plate
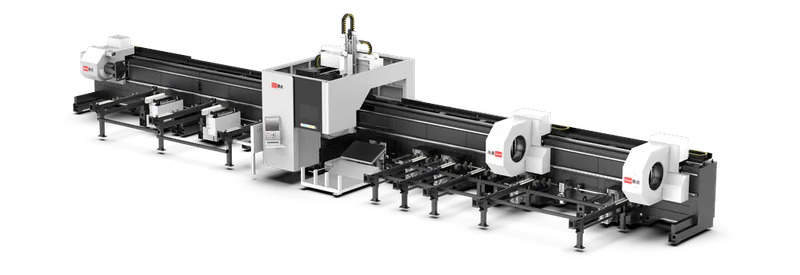
The LHM Series is a gantry laser machine that cuts both heavy profiles and plate, for structural steelwork fabricators. It can be configured with 1, 2 or 3 stations. 12–40 kW of power, H/I/U/L profiles up to 1,200×600 mm, 5-axis bevel cutting (±45°, V/Y/X/K bevels) and a Tekla-compatible workflow.
- Laser power: 12–40 kW
- Max. profile: 1,200×600 mm (12 m length)
- Bevel: 5-axis · ±45° (V/Y/X/K)
- Software: Tekla-compatible
Why the LHM Series
What it handles
Profiles up to 1,200×600 mm and plate up to 12,000×3,000 mm on the same machine: I-beams and H-beams, channel, angle and plate. All the profiles and plate for a structure go through a single line.
The LHM Series difference
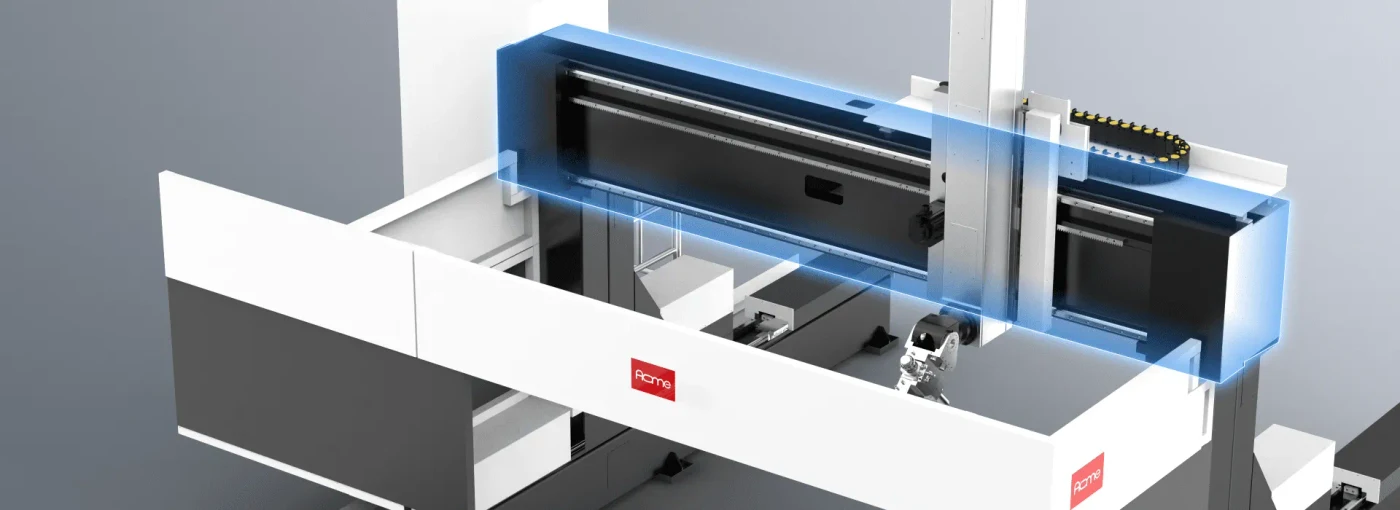
Bed structure
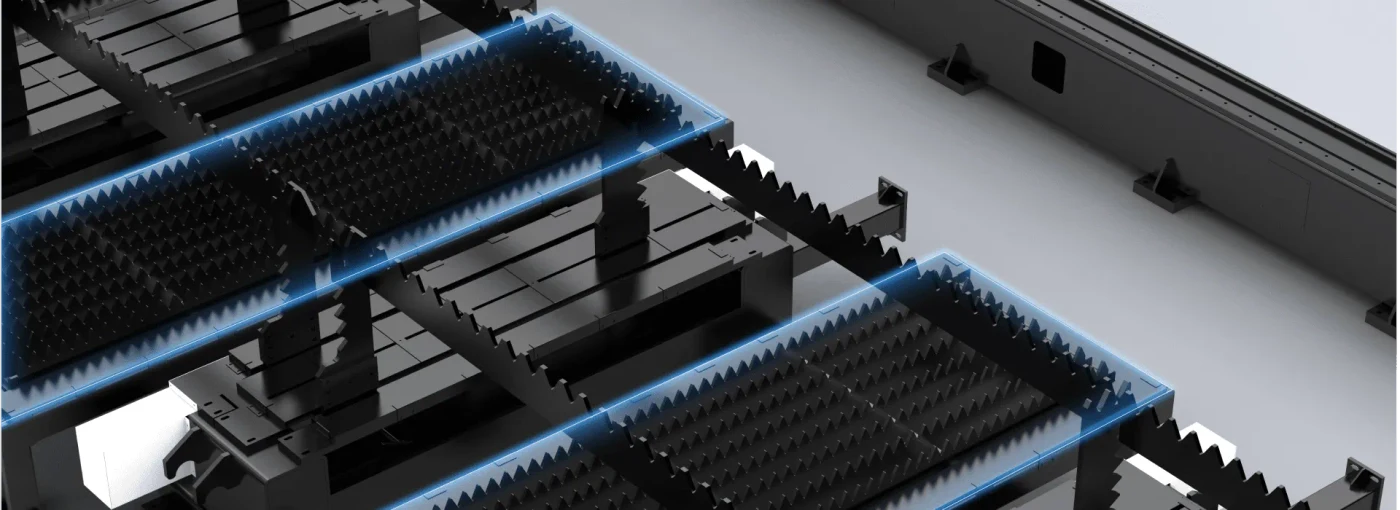
The bed sits on floor rails and is assembled from sections: it can be customised and is easier to transport, even in large formats. Because it is separate from the work table, it suffers less wear when heavy parts are cut.
LHM Series
LHM Series in our own production facility in Cluj-Napoca — 12 m profiles + plate on a gantry, combined line.
Inside the LHM Series
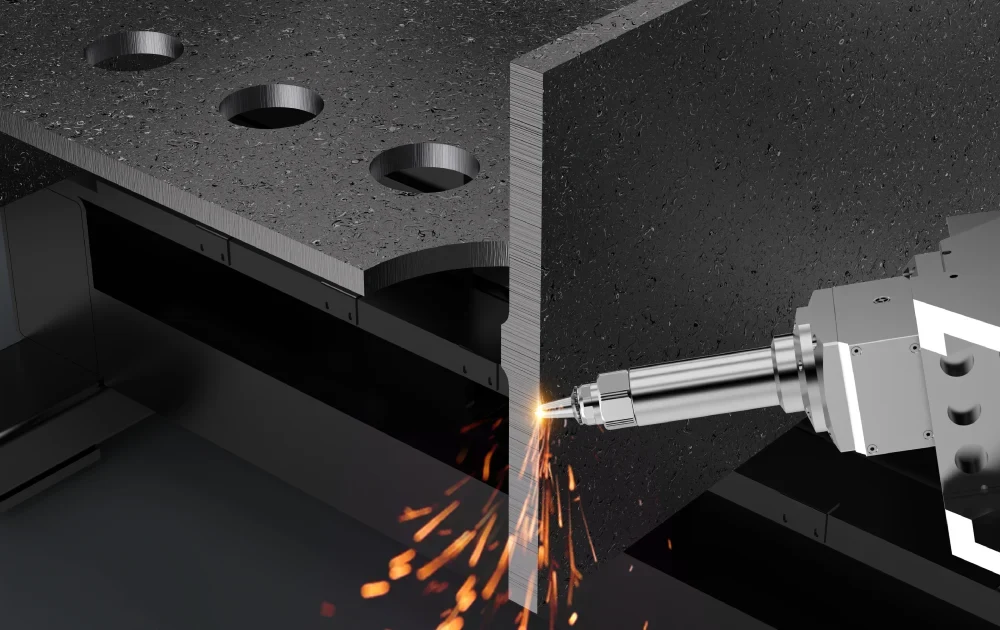
5-axis 3D bevel cutting
The 5-axis cutting head prepares the weld joint at ±45°, in V, Y, X and K geometries or as a compound bevel, on profiles and on plate. Parts fit better at assembly and need less grinding.
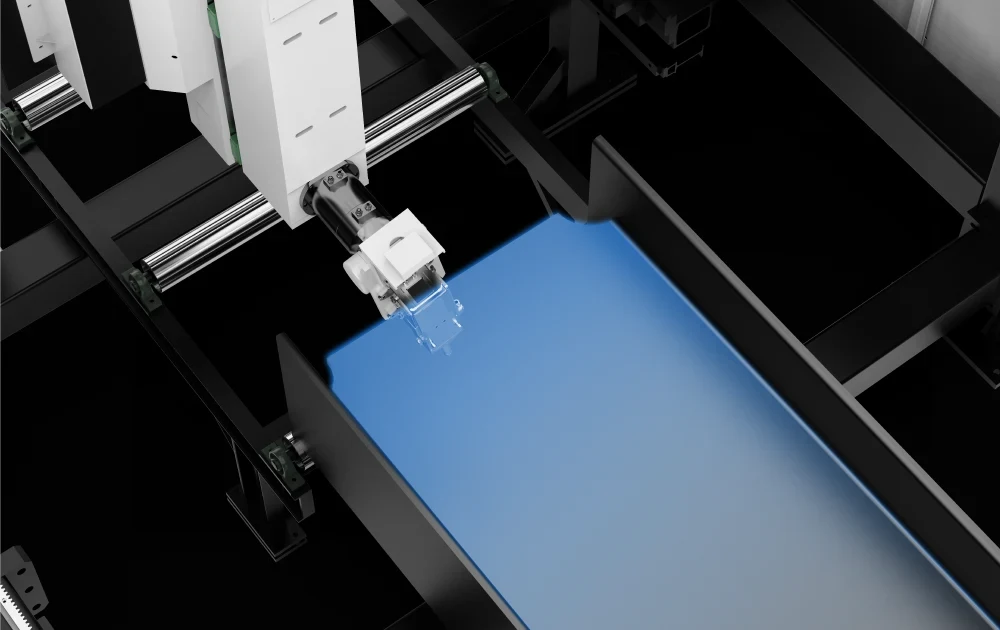
Ultra-short remnant
The head steers around the clamping zone and cuts from the minimum safe distance, so the profile end left over is as short as possible. Material loss is minimal and costs fall.
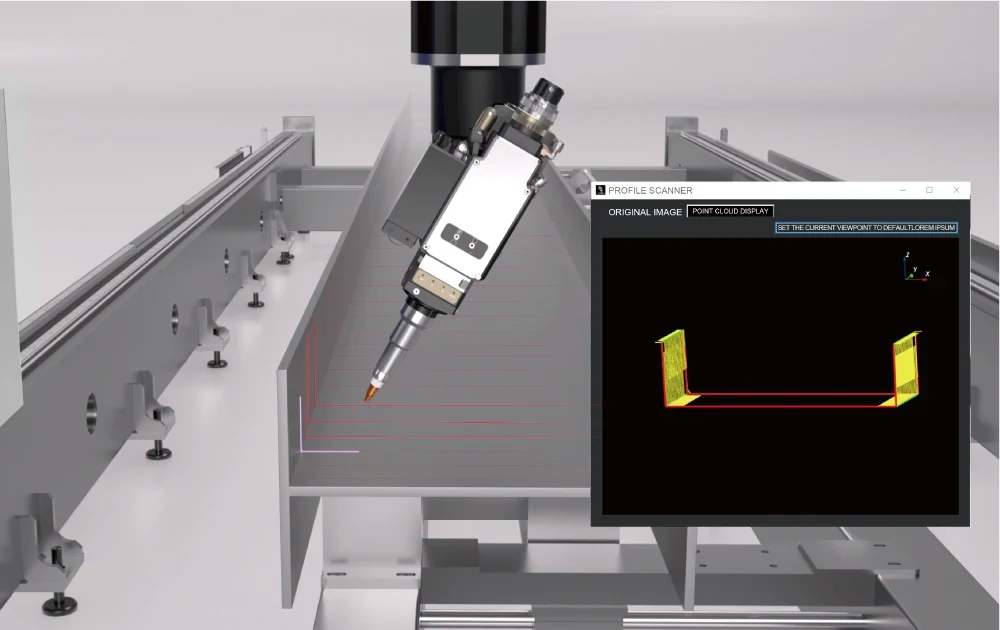
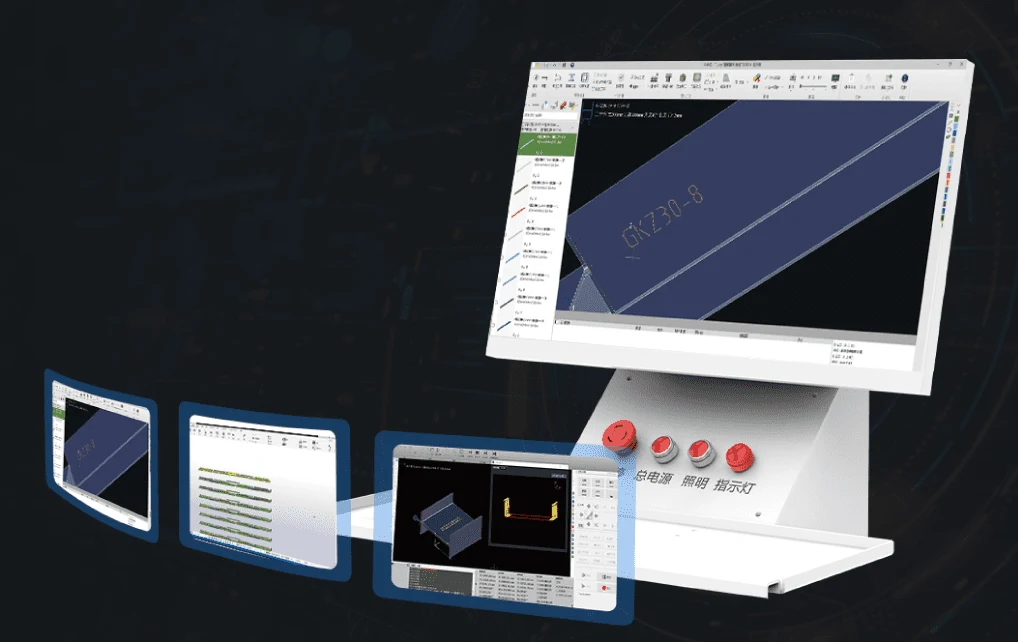
Visual alignment
A contour scanner measures the deviation between the actual part and the drawing and compensates for it. Processing stays accurate and stable, without offset cuts or skewed holes.
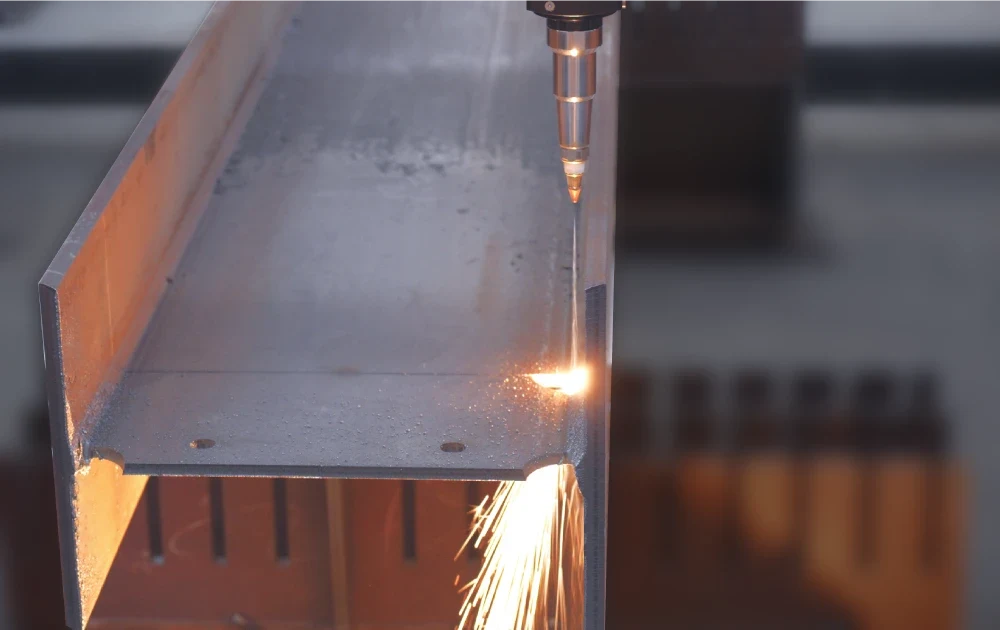
Height control — cutting in any position
The system allows cutting at a fixed height and with height control even beyond the edge of the plate, while the head keeps the optimum distance from the material anywhere on the working area.
Easy to commission
Parallel stations
It can be configured with 1, 2 or 3 stations: while one cuts, the next is loaded and unloaded. Time is saved on loading and unloading, and the profile can be processed in sections or as a whole.
Explore ACME technology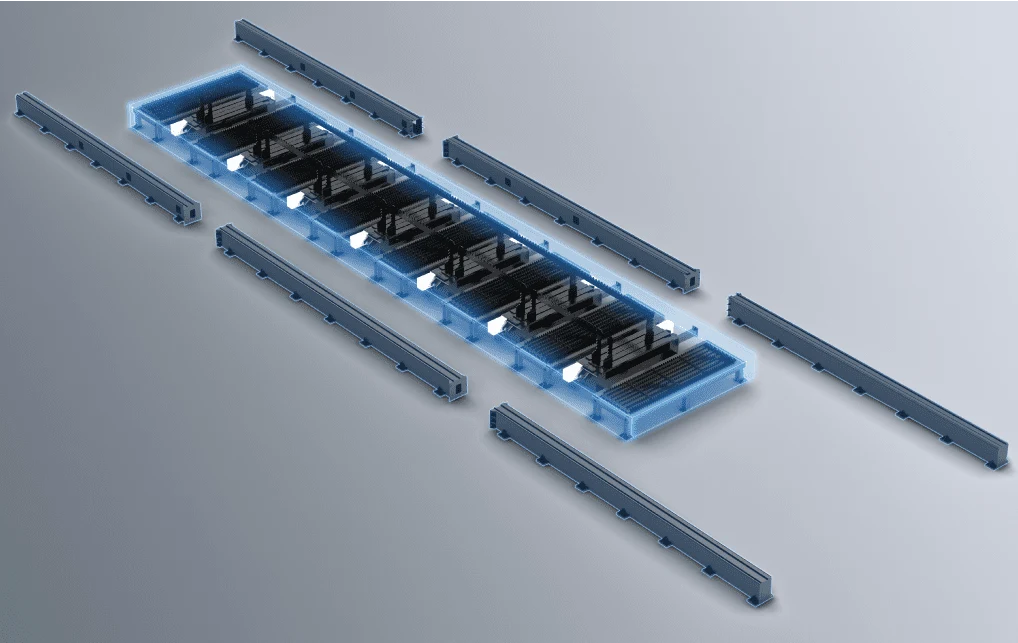
One machine, multiple functions
The same machine handles profile cutting, bevel cutting on profiles and plate, and 2D cutting, without separate machines. Fume extraction is zoned: on profiles, extraction follows the head; on plate, fumes are drawn through the grid; a full enclosure is optional. Production is cleaner and safer.
See our services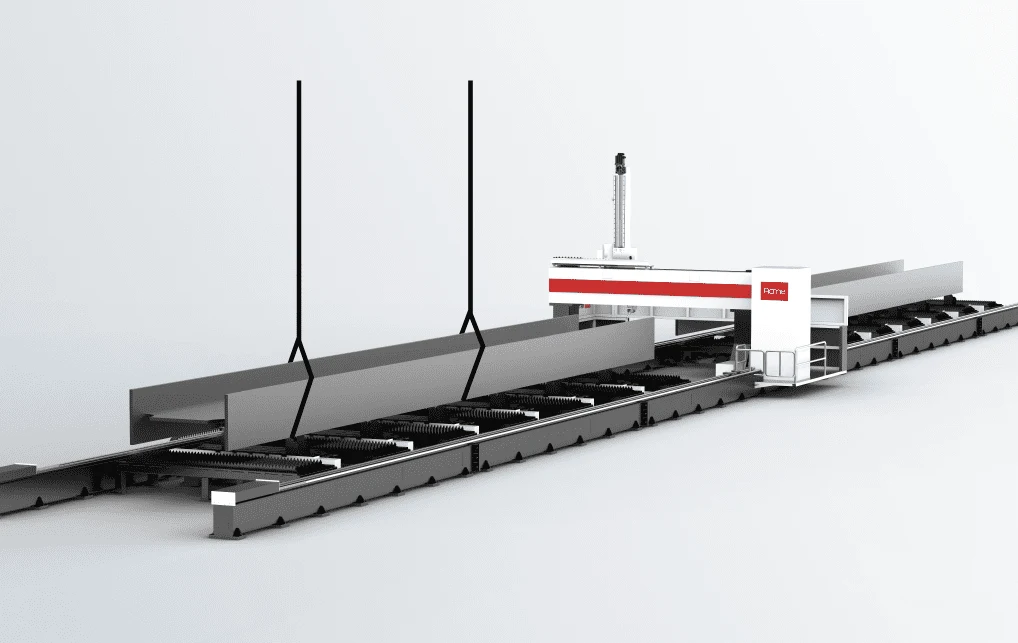
Separately mounted components
The laser source, the water chiller and the machine bed are designed as separate units, each fixed to the floor. The bed is under less stress in operation, and cutting keeps its accuracy over time.
Talk to a specialistWhy a local dealer
Authorised dealer
ACME's authorised partner for Romania, not just a reseller.
Service by our own technicians
Commissioning, maintenance and repairs, carried out by our own technicians.
Parts in stock in Romania
Nozzles, lenses and critical components held in Romania — days, not weeks.
We use them ourselves
We run 2 ACME machines in our own manufacturing business.
Technical data
Official ACME specifications — 3 configurations by number of stations. H12012 = 12 m profile gantry; +P6025 / +P6030 = additional plate station.
| Model | H12012 (1 station) | H12012+P6025 (2 stations) | H12012+H12012+P6030 (3 stations) |
|---|---|---|---|
| Laser power | 12–40 kW | 12–40 kW | 12–40 kW |
| Total weight | 17 t | 28 t | 30 t |
| Max. profile (W×H) | 1,200 × 600 mm | 1,200 × 600 mm | 1,200 × 600 mm |
| Min. profile (W×H) | 200 × 100 mm | 200 × 100 mm | 200 × 100 mm |
| Max. plate size (L×W) | — (profiles only) | 12,000 × 2,500 mm | 12,000 × 3,000 mm |
| Machine dimensions (mm) | L 18,700 × W 7,600 H 5,000 | L 23,000 × W 7,600 H 5,000 | L 43,000 × W 7,600 H 5,000 |
| Bevel | 5-axis, ±45° — V / Y / X / K bevels, compound bevels on profiles and plate | ||
| Software | Tekla-compatible — component data brought into nesting and processing | ||
| Stations | 1, 2 or 3 | ||
| Cutting functions | profile cutting, profile bevel cutting, plate bevel cutting, 2D cutting | ||
| Profile types | I-beam / H-beam, channel, angle and other structural profiles | ||
- Configuration
- H12012 (1 station)
- Laser power
- 12–40 kW
- Total weight
- 17 t
- Max. profile (W×H)
- 1,200 × 600 mm
- Min. profile (W×H)
- 200 × 100 mm
- Max. plate size (L×W)
- — (profiles only)
- Machine dimensions (mm)
- L 18,700W 7,600H 5,000
- Stations
- 1, 2 or 3
- Bevel
- 5-axis, ±45° — V / Y / X / K bevels, compound bevels on profiles and plate
- Software
- Tekla-compatible — component data brought into nesting and processing
- Cutting functions
- profile cutting, profile bevel cutting, plate bevel cutting, 2D cutting
- Profile types
- I-beam / H-beam, channel, angle and other structural profiles
- Configuration
- H12012+P6025 (2 stations)
- Laser power
- 12–40 kW
- Total weight
- 28 t
- Max. profile (W×H)
- 1,200 × 600 mm
- Min. profile (W×H)
- 200 × 100 mm
- Max. plate size (L×W)
- 12,000 × 2,500 mm
- Machine dimensions (mm)
- L 23,000W 7,600H 5,000
- Stations
- 1, 2 or 3
- Bevel
- 5-axis, ±45° — V / Y / X / K bevels, compound bevels on profiles and plate
- Software
- Tekla-compatible — component data brought into nesting and processing
- Cutting functions
- profile cutting, profile bevel cutting, plate bevel cutting, 2D cutting
- Profile types
- I-beam / H-beam, channel, angle and other structural profiles
- Configuration
- H12012+H12012+P6030 (3 stations)
- Laser power
- 12–40 kW
- Total weight
- 30 t
- Max. profile (W×H)
- 1,200 × 600 mm
- Min. profile (W×H)
- 200 × 100 mm
- Max. plate size (L×W)
- 12,000 × 3,000 mm
- Machine dimensions (mm)
- L 43,000W 7,600H 5,000
- Stations
- 1, 2 or 3
- Bevel
- 5-axis, ±45° — V / Y / X / K bevels, compound bevels on profiles and plate
- Software
- Tekla-compatible — component data brought into nesting and processing
- Cutting functions
- profile cutting, profile bevel cutting, plate bevel cutting, 2D cutting
- Profile types
- I-beam / H-beam, channel, angle and other structural profiles
Specifications are subject to change as the manufacturer develops its machines. We confirm the exact values for your configuration in your quotation.
Who this machine is built for
Three stations can work side by side: while one cuts a 12-metre profile, the next is being loaded, and the third takes the plate. In a single pass, the profile gets its holes, markings and bevels and is cut to size.
The head works on 5 axes, so the weld preparation is cut at ±45°, in V, Y, X or K, on both profile and plate. The Tekla-compatible workflow takes component data into nesting without redrawing.
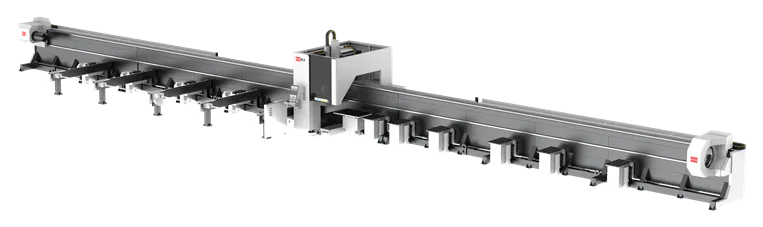
The ST and DT Series pair sheet with tube; the LHM pairs plate with heavy profiles, up to 1,200×600 mm. Below 200×100 mm, the profile no longer fits the machine.
Questions about the LHM Series
What profiles can the LHM Series cut, and in what sizes?
The LHM Series cuts structural profiles from 200×100 mm up to 1,200×600 mm (width × height), in 12 m lengths: I-beams and H-beams, channel, angle and other structural profiles. In a single pass, the profile gets its holes, marking, scribing and bevels and is cut to length; the interlocking joints are cut in the same pass. Profiles smaller than 200×100 mm do not fit the machine.
Can the LHM Series cut plate as well, not just profiles?
Yes. The LHM Series cuts plate on the same machine, at a station separate from the profile station: the 2-station configuration (H12012+P6025) covers formats up to 12,000×2,500 mm, and the 3-station configuration (H12012+H12012+P6030) up to 12,000×3,000 mm. The 5-axis head also bevels plate at ±45°, so the weld preparation comes off the machine ready. A single machine covers profile cutting, 2D plate cutting and bevel cutting on both.
How does the LHM Series cut weld-prep bevels?
The LHM Series has a 5-axis cutting head that prepares the weld joint at ±45° directly during cutting, without a separate operation. The geometries are V, Y, X and K, plus the compound bevel, on both profiles and plate. Holes, marking, scribing and cutting to length are done in the same pass, so parts fit together well at assembly and need less grinding.
Is the LHM Series compatible with Tekla?
Yes. The LHM Series is Tekla-compatible: component data is brought into the nesting and processing workflow without redrawing. Programming is faster, and nesting makes better use of the material. Tekla compatibility, together with H/I/U/L profiles up to 1,200×600 mm, makes the LHM Series suited to the structural steelwork industry.
What laser power does the LHM Series have?
All three LHM Series configurations have 12–40 kW of laser power: H12012 (1 station), H12012+P6025 (2 stations) and H12012+H12012+P6030 (3 stations). Power does not depend on the number of stations. The final value is chosen according to your materials, thicknesses and production volume.
What do the 1-, 2- or 3-station configurations mean on the LHM Series?
The number of stations shows how many working zones the LHM Series has. The H12012 has a single station, for profiles only. The H12012+P6025 adds a plate station, while the H12012+H12012+P6030 has two profile stations and one plate station. The stations operate in sequence or in parallel: while one cuts, the next is loaded and unloaded, and the profile can be processed in sections or as a whole.
What footprint and weight does the LHM Series have?
The LHM Series footprint grows with the number of stations, while the width (7,600 mm) and height (5,000 mm) stay the same. The 1-station configuration (H12012) is 18,700 mm long and weighs 17 t, the 2-station configuration (H12012+P6025) 23,000 mm and 28 t, and the 3-station configuration (H12012+H12012+P6030) 43,000 mm and 30 t.
Other machines we recommend
Where it is used
ACME units installed worldwide
countries & regions with installations
machine series in the range
machine models in the catalogue
Interested in the LHM Series?
Tell us about your application — profile types (H/I/U/L), maximum sizes, whether you also have plate to cut, the power you want (12–40 kW) and the number of stations (1, 2 or 3). We will reply in writing with the configuration we recommend.
Free consultation · Authorised ACME dealer · Installation and service in Romania